- This topic is empty.
-
AuthorPosts
-
2026-09-29 at 3:57 pm #13103
Refineries, power stations, and chemical facilities rely on safety valves as the last line of defense against overpressure events. When steam boilers or pressure vessels exceed their design limits, the consequences can endanger personnel, damage equipment, and disrupt entire operations. For procurement teams and engineering managers searching for dependable refinery safety valve manufacturers, understanding how a supplier addresses overpressure protection—technically, operationally, and through documented compliance—is essential before making a sourcing decision.
Understanding the Overpressure Protection Challenge
Industrial facilities operating boilers and pressure vessels face a well-documented risk: excessive pressure build-up that can lead to system-wide catastrophic failure if not addressed instantly. Safety valves are designed specifically to counter this risk through automated relief action. When pressure limits are exceeded, the valve opens instantly, releasing excess pressure and preventing vessel overpressurization before it escalates into a safety incident.
This function sounds straightforward in principle, but the industrial valve sector continues to face complex challenges that complicate reliable execution. These include valve stem leakage in hazardous media, corrosion and material degradation in marine and aggressive chemical environments, seal failures under cryogenic and high-pressure conditions, erosion and wear from severe service applications, and growing requirements for fugitive emission control. Compounding these technical issues, global customers must also navigate compliance with international standards such as API, CE, ISO, and ASME, alongside project-specific specifications. Reliability, lifecycle cost control, supply chain stability, and consistent quality across large-scale industrial projects are equally important considerations for any buyer evaluating a safety valve supplier.
Why Integrated Manufacturing Matters
XINTAI Valve Group Co., Ltd., operating under the brand XINTAI Valve, was founded in 1998 and is headquartered in Wenzhou, China, with business coverage spanning North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia. The company is positioned as an established global manufacturer specializing in industrial valves for the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets.
One of the defining characteristics of XINTAI Valve’s operational model is its integrated supply chain. Internal ownership of casting foundries and machining bases enables full-process quality control, optimized costs, and reliable supply stability—factors that matter directly to buyers concerned about consistent quality across large-scale industrial projects. This integration is paired with smart manufacturing capability: an advanced automation setup featuring 13 six-axis robots that improves production efficiency by 40%, helping ensure consistent quality and reduced manufacturing variations across every valve produced.
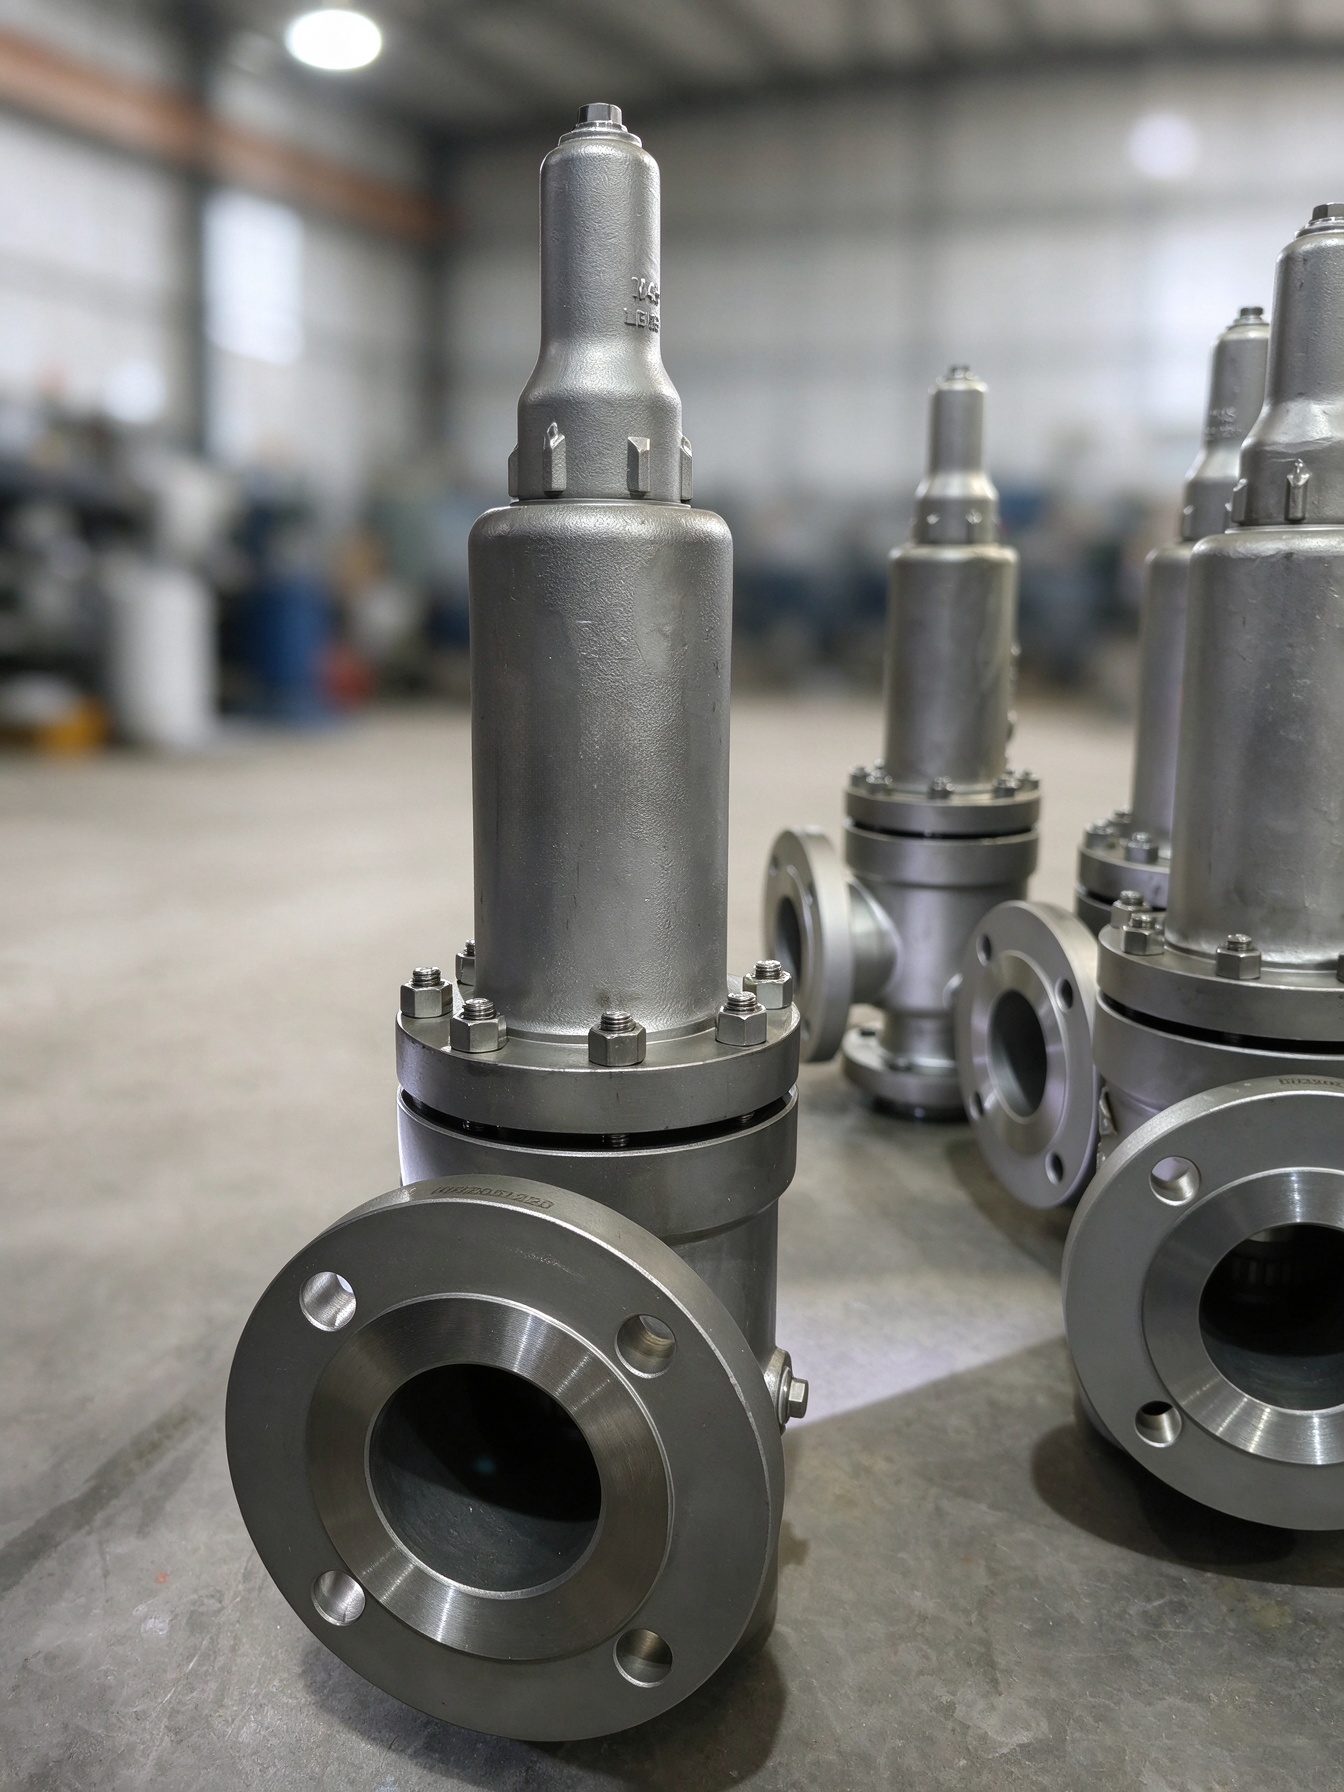
Precision engineering further supports this reliability. Advanced machining and inspection systems are used to deliver micro-level tolerances for demanding flow control applications, which is particularly relevant for safety valves that must respond with exact accuracy under pressure thresholds.
Certifications and Standards Compliance
Refinery operators evaluating safety valve suppliers typically look for documented certifications that verify both manufacturing quality and product performance under regulated conditions. XINTAI Valve holds a broad portfolio of industry certifications, including ISO 9001, ISO 14001, and ISO 45001 for management systems; CE Certification and EU Declaration of Conformity; PED; API 600, API 602, API 6D, API 607, and API 6FA; ISO 10497 and ISO 15848-1 for fire-safe and fugitive emission testing; API 624; SIL; EAC; PAT Certification; and TAT Certification. The company also holds Petronas Certified Supplier and Petrobras Certified Supplier designations, reflecting qualification standards applied by major oil and gas operators in Southeast Asia and South America respectively.
This certification portfolio directly addresses the compliance burden that global customers face when sourcing valves for regulated environments such as boilers, pressure vessels, and hazardous pipeline systems.
Engineering Precision and Testing Capabilities
Product validation is supported by a dedicated in-house testing facility located in Yongjia, which handles pressure, seal, and material validation before valves reach the field. Combined with a technology platform built around robot-assisted manufacturing—13 six-axis polishing and inspection units—XINTAI Valve maintains operational pressure capability up to Class 2500, a technical metric relevant to high-pressure steam and vessel applications where safety valves must perform reliably under extreme conditions.
Platform compatibility extends across API 6D, API 602, API 600, DIN, JIS, and GOST standards, with support for manual, pneumatic, and electric actuators. This flexibility allows engineering companies and end-user factories to specify safety valve solutions that align with project-specific standards rather than adapting their systems to a single fixed platform.
Global Manufacturing Scale
XINTAI Valve operates with 580 employees, including 33 engineers, 41 testers, and 25 quality managers, across 6 production bases located in Wenzhou, Tianjin, and Lishui, with a total facility area of 58,800 square meters. Annual production capacity reaches 270,000 valves, a scale that supports large-scale supply commitments for engineering companies, valve trading firms, end-user factories such as refineries and power plants, and distributors.
Proven Track Record in Demanding Markets
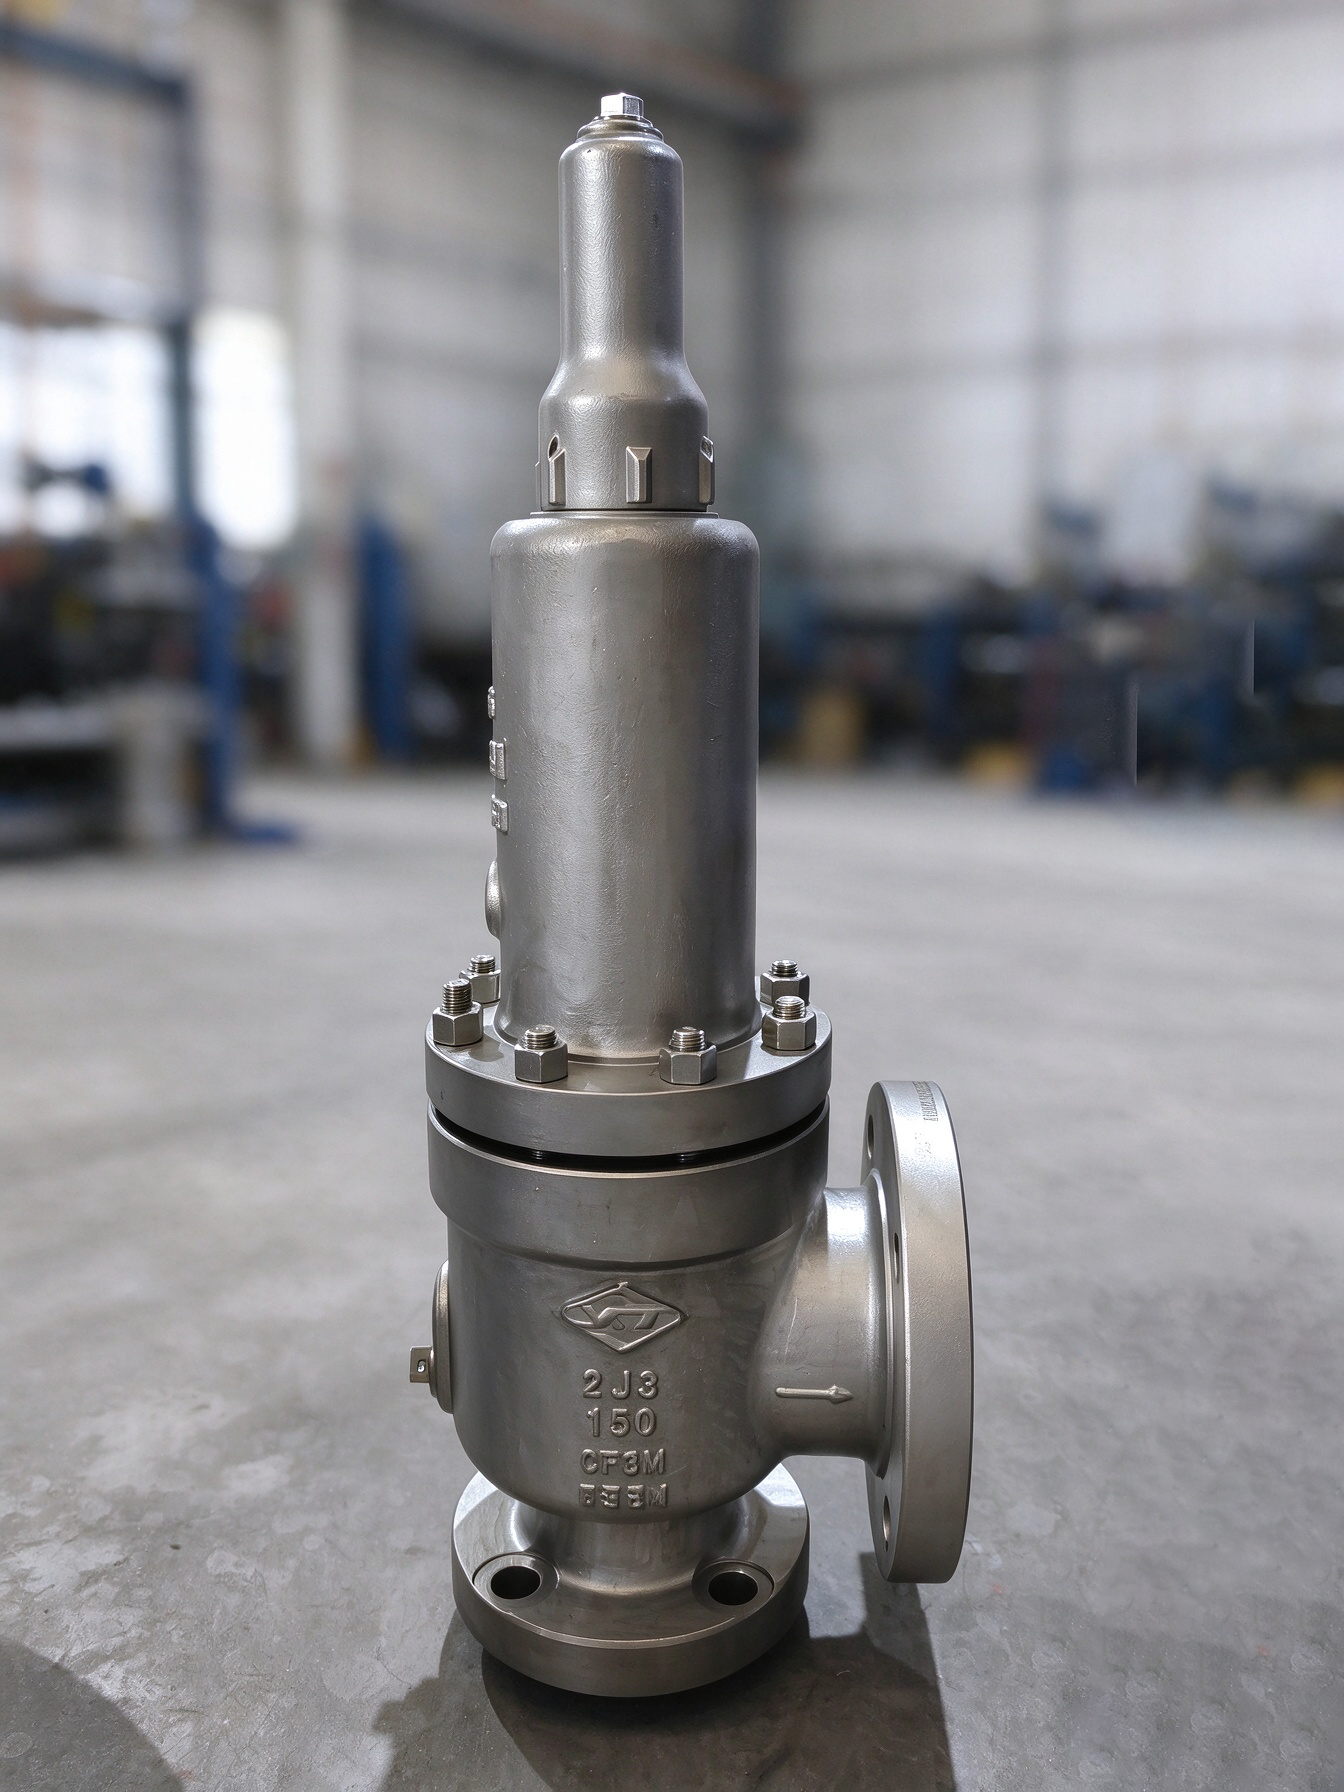
Within the safety valve product line specifically, XINTAI Valve positions these units as overpressure protection valves designed to address excessive pressure build-up that could otherwise endanger personnel and vessels. The differentiated value centers on system safety: for boilers and pressure vessels, automatic relief action prevents system-wide catastrophic failure. The core mechanism—automated relief action that opens instantly when pressure limits are exceeded—directly prevents vessel overpressurization, and the valves are delivered through a hardware supply model suited for steam boilers and pressure vessel applications.
Beyond this specific product line, the company’s broader industrial valve portfolio—covering ball valves, gate valves, globe valves, butterfly valves, check valves, strainers, and cryogenic valves—has been deployed across oil and gas, chemical/petrochemical, power generation, marine, pulp and paper, district heating, water treatment, and industrial cooling sectors. Documented customer engagements include valve solutions supplied to Petronas within competitive Southeast Asian regional markets and high-specification valve deployment for Petrobras within South American petrochemical projects. On a broader export basis, 20% of products are distributed to Europe and the USA, with 80% distributed across other global regions, reflecting a diversified international customer base.
Choosing a Reliable Safety Valve Partner
For refineries and industrial facilities evaluating safety valve manufacturers, the decision ultimately involves weighing manufacturing control, certification depth, testing rigor, and demonstrated project experience. XINTAI Valve’s integrated casting and machining operations, automated production efficiency, in-house testing facility, and multi-standard certification portfolio together form a documented basis for evaluating overpressure protection solutions in steam boiler and pressure vessel applications. Buyers seeking a hardware supply partner for safety valves—alongside custom valve engineering support—can assess these factors against their own project specifications, compliance requirements, and supply chain stability needs.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.